High-Purity Protein Fortification Portfolio
Explore our premium grade plant-based and specialty protein isolates engineered for food, beverage, and dietary supplement formulations.
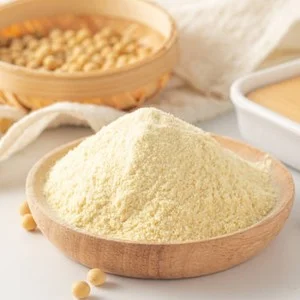
Professional Manufacturer High Quality Soybean Flour Soy Protein Powder Natural Organic Price Is Beautiful
View Technical Specs
ISO Halal Kosher Pumpkin 60%Protein Powder Premium Pumpkin Seed Protein For Supplements
View Technical Specs
High Quality Organic Oat Protein 80% Oat Protein Powder
View Technical Specs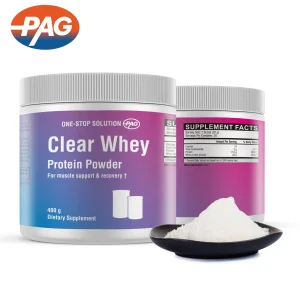
Private Label Made In Germany Sports Supplements Energy Booster Support 400G Clear Whey Protein Powder
View Technical Specs
Mung Bean Protein for Meat Alternatives | Textured Vegetable Protein (TVP) Format
View Technical Specs
Organic 100% Plant Based Sunflower Seed Protein Powder 50% 100%
View Technical Specs
China Protein Manufacturer Supply Hot Sales 100%Pure Natural Free Sample 90%Protein Green Faba Bean Powder
View Technical Specs
OEM Organic Pea Protein Isolate Powder Private Label Adult Supplement Customizable 1-2 Times Daily 500mg/1000mg
View Technical SpecsGlobal Protein Fortification Market Overview (2025–2030)
Understanding shifting consumer demands, nutritional metrics, and formulation engineering in modern protein enrichment.
Nutritional Density & PDCAAS
Modern protein fortification focuses heavily on achieving optimal Protein Digestibility-Corrected Amino Acid Scores (PDCAAS) and Digestible Indispensable Amino Acid Scores (DIAAS). Formulators blend pulse, cereal, and seed proteins to deliver complete essential amino acid profiles matching traditional dairy standard benchmarks.
Clean-Label Transformation
Global procurement teams prioritize physical extraction, enzyme-assisted concentration, and organic-certified processes over traditional chemical isolation. Eliminating synthetic additives, hexanes, and allergens is key to maintaining consumer trust across Western European and North American retail channels.
Functional Versatility
Protein ingredients are no longer evaluated solely for protein percentage. Critical functional parameters include water-binding capacity, oil absorption index, emulsion stability, cold-water solubility, thermal gelation, and organoleptic neutrality across high-temperature short-time (HTST) food processing.
Top 10 Global Protein Fortification Manufacturers & Suppliers
An objective benchmark of leading global suppliers evaluating manufacturing scale, technical R&D, portfolio breadth, and supply integrity.
| Manufacturer / Brand | Primary Protein Specializations | Key Strengths & R&D Capabilities | Core Application Markets |
|---|---|---|---|
| Dongguan Tsrel Biology Co., Ltd. | Soy, Pea, Faba Bean, Mung Bean, Pumpkin, Oat, Rice & Specialty Plant Proteins | Full-spectrum plant isolation, custom enzymatic hydrolysis, high-moisture TVP extrusion, complete OEM/ODM formulation services. | Global Sports Nutrition, Meat Alternatives, RTD Beverages, Functional Bakery & Supplements |
| ADM (Archer Daniels Midland) | Soy Isolate, Wheat Gluten, Textured Plant Proteins | Extensive global agricultural footprint, deep flavor-masking capabilities, massive bulk volume supply stability. | Commercial Food Processing, Animal Nutrition, Industrial Foodservice |
| Cargill, Incorporated | Pea Protein Isolates, Soy Concentrates, Corn Protein | Advanced supply chain logistics, high-clarity liquid solubility, extensive regulatory advocacy across continents. | Dairy Alternatives, Confectionery, Clinical Nutrition |
| Roquette Frères | Yellow Pea Protein Isolates & Hydrolysates | Pioneer in yellow pea fractionation, high thermal stability formulations, sustainable European crop sourcing. | Specialized Infant Formula, Sports Performance, Vegan Snacks |
| Kerry Group plc | Hydrolyzed Proteins, Plant Peptides, Yeast Extracts | Sensory science integration, taste-masking technologies, tailor-made bioactive peptide development. | Functional Beverages, Clinical Nutrition, Premium Consumer Brands |
| DuPont Nutrition & Biosciences (IFF) | Soy Protein Isolates, Structured Vegetable Proteins | Microbial enzyme pairings, textured protein structure modeling, massive global application centers. | Plant-based Meats, High-Protein Bakery, Processed Meats |
| Cosucra Groupe Warcoing | Chicory Root Fiber & Pea Protein Isolates | Non-GMO specialty pea extraction, sustainable closed-loop processing, clean-label digestive health solutions. | Weight Management, Gut Health Products, Clean Bakery |
| Glanbia Nutritionals | Dairy Whey Protein Concentrates, Isolate & Plant Blends | Sports nutrition leadership, micro-filtered cold process whey isolate, cross-functional powder blending. | Bodybuilding Supplements, Active Nutrition, Medical Nutrition |
| FrieslandCampina Ingredients | Bioactive Whey Micro-Fractionations, Caseinates | Infant-grade safety standards, high-purity bioactive whey peptides, specialized micro-filtration technology. | Early Life Nutrition, Senior Health, Specialized Clinical Diets |
| Angel Yeast Co., Ltd. (Angeopro) | Fermented Yeast Protein Powder Isolate | Sustainable precision fermentation, eco-friendly footprint, non-allergenic complete amino acid profile. | Alternative Protein Supplements, Vegan Sports Powders |
Dongguan Tsrel Biology Co., Ltd.
Pioneering Sustainable Plant Protein Solutions for Global Food & Nutritional Industries
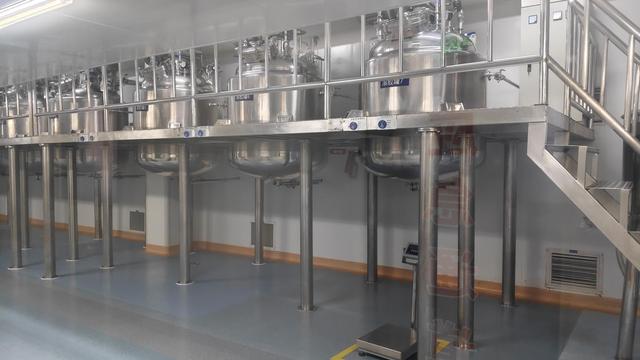
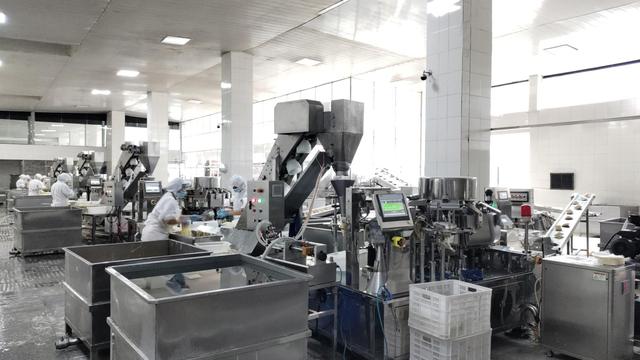
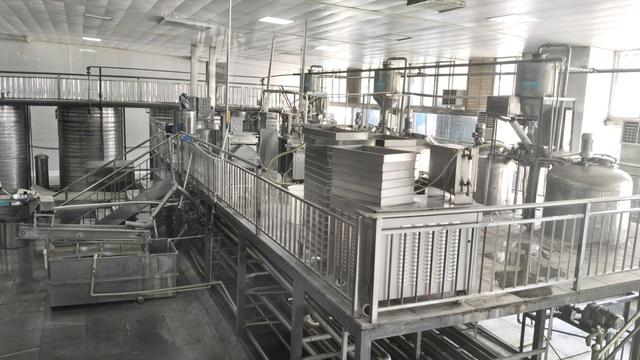
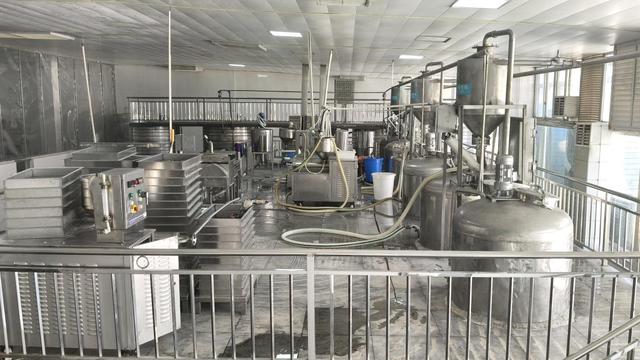
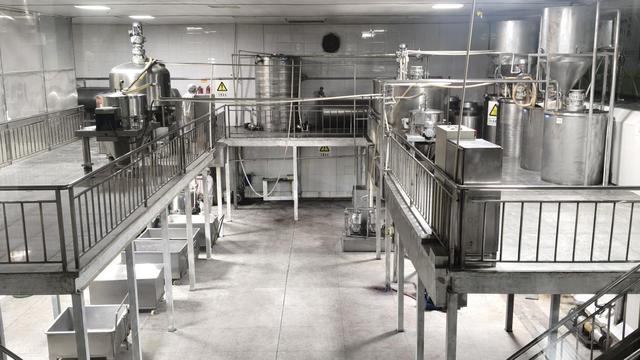
Dongguan Tsrel Biology Co., Ltd. is a professional China vegetal protein manufacturer specializing in the research, development, production, and supply of high-quality plant protein ingredients for food, beverage, and nutritional applications. With a strong focus on innovation, sustainability, and quality assurance, the company is dedicated to providing reliable plant-based ingredient solutions to customers worldwide.
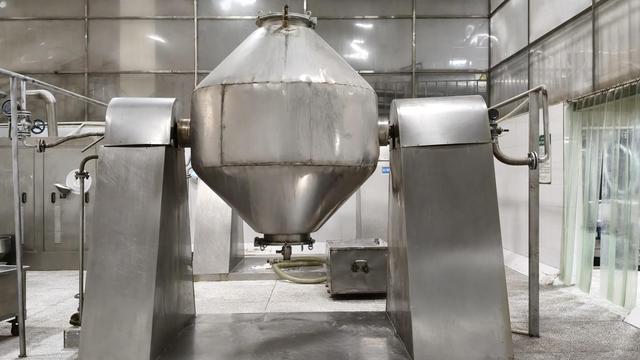
Equipped with advanced manufacturing facilities and modern processing technologies, Dongguan Tsrel Biology offers a comprehensive range of vegetal proteins, including soy protein, pea protein, rice protein, wheat protein, and other specialty plant proteins. These ingredients are widely used in functional foods, nutritional supplements, sports nutrition products, dairy alternatives, meat alternatives, beverages, bakery products, and health food applications.
Innovation is a key driving force behind the company's growth. Supported by an experienced research and development team, Dongguan Tsrel Biology continuously explores new technologies and application solutions to meet the evolving demands of the global food and nutrition industries. The company also provides customized ingredient solutions to help customers optimize product formulations, improve nutritional profiles, enhance texture, and create clean-label products.
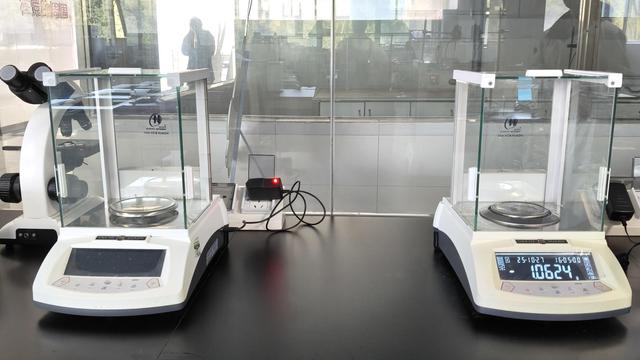
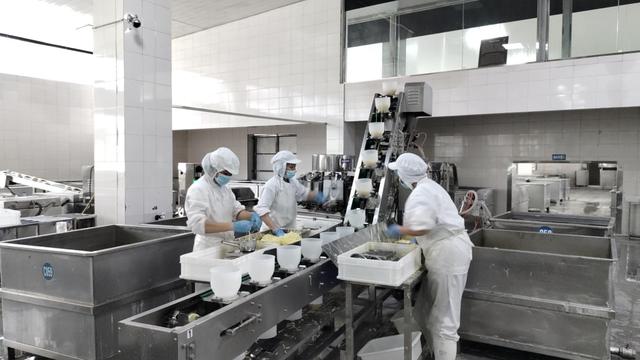
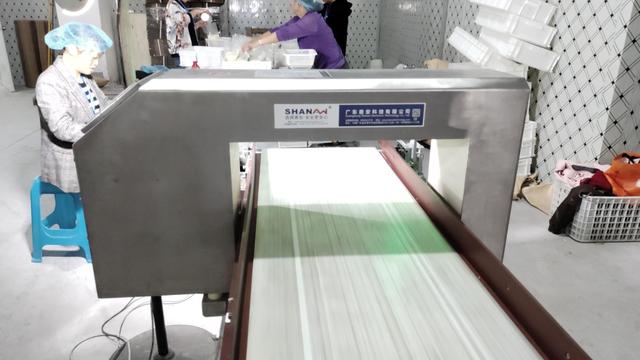
Quality and food safety are integrated into every stage of production. From raw material sourcing and processing to final testing and packaging, strict quality control procedures are implemented to ensure product consistency, purity, safety, and compliance with international standards. This commitment enables the company to deliver dependable products that meet the rigorous requirements of global customers.
With customer satisfaction at the center of its operations, competitive manufacturing capabilities, stable supply chains, and professional technical support, Dongguan Tsrel Biology Co., Ltd. has established long-term partnerships with food manufacturers, distributors, and brand owners across international markets. The company remains committed to advancing sustainable nutrition through innovative plant protein solutions for the global marketplace.
Supply Chain Capabilities by the Numbers
Delivering high-capacity, standardized ingredient solutions to over 50 countries worldwide.
China's Plant Protein Supply Chain Superiority
Why international food giants leverage China's ecosystem for raw material sourcing and scale processing.
Agronomic Upstream Proximity
China commands extensive agricultural cultivation regions for non-GMO soybeans, yellow peas, faba beans, and specialty crops in Northeast and Northern agricultural belts. Close geographic proximity between harvesting centers and processing plants reduces transportation degradation and preserves cellular protein structural integrity.
Advanced Ultrafiltration & Drying Technology
Modern Chinese protein factories utilize state-of-the-art ceramic membrane ultrafiltration, multi-stage spray drying, and enzymatic hydrolysis equipment. This industrial sophistication permits exact control over particle size distribution (mesh sizes 80–300) and protein purity ratios reaching 90%+ in commercial isolate lines.
Unrivaled Cost-to-Performance Ratio
Through fully integrated industrial energy infrastructure, automated bulk material handling, and end-to-end byproduct utilization (starching, dietary fiber recovery, solubles concentration), Chinese suppliers provide world-class quality at capital-efficient cost points ideal for global B2B expansion.
Global Enterprise B2B Purchasing Framework
Essential quality metrics, testing parameters, and physical-chemical requirements required by international buyers.
Physicochemical & Analytical Specifications
- Protein Assay (Dry Basis): Minimum 80% to 90% via Kjeldahl or Dumas methods (N x 6.25).
- Moisture Content: Kept strictly under 6.0% - 8.0% to guarantee microbial stability and inhibit clumping during bulk storage.
- Ash Content: Controlled below 5.5% to preserve organoleptic clarity and minimize metallic off-flavors.
- Bulk Density: Standardized loose and tapped density (0.35 - 0.55 g/mL) for efficient high-speed container packaging.
- Solubility Index (NSI / PDI): Tailored Nitrogen Solubility Index ranging from low NSI (for textured meats) to high NSI >85% (for RTD beverages).
Microbiological Safety & Traceability Safeguards
- Total Plate Count (TPC): < 10,000 CFU/g under stringent cleanroom hygienic manufacturing protocols.
- Pathogen Free Guarantee: Negative testing for Salmonella, Listeria monocytogenes, E. coli, and Staphylococcus aureus per 25g/375g analytical samples.
- Heavy Metal Compliance: Lead < 0.2 mg/kg, Arsenic < 0.1 mg/kg, Cadmium < 0.1 mg/kg, Mercury < 0.05 mg/kg meeting EU/FDA strict food limits.
- Allergen Segregation: Dedicated line processing options for soy-free and gluten-free plant isolates (e.g., Pea, Rice, Pumpkin, Faba).
Global Compliance, Certification & Regional Support
Navigating cross-border food regulations, labeling compliance, and religious certification standards.
Religious & Dietary Certifications
Full availability of Kosher (Pareve), Halal, Vegan Society, and Non-GMO Project Verified certifications ensuring seamless global distribution across diverse consumer demographics.
EFSA & US FDA Compliance
Detailed Certificate of Analysis (COA), safety data sheets (SDS), technical data sheets (TDS), GRAS status documentation, and allergen declarations aligned with EU 1169/2011 regulations.
Custom OEM/ODM Private Labeling
Flexible packaging formats ranging from 20kg bulk kraft multi-wall bags with PE liners to customer-branded retail tubs, pouches, and stick-packs with custom flavor application.
Warehousing & Local Logistics
Standardized export packaging, temperature-controlled containerized shipping, fast customs clearance handling, and local stock replenishment hubs across key international ports.
Localized Industry Application Scenarios
Tailored protein functional solutions optimized for specific end-use food and beverage matrix challenge zones.
1. Ready-To-Drink (RTD) Beverages
Formulation Challenge: Sedimentation, astringency, gritty mouthfeel, phase separation during heat processing.
Ingredient Solution: Highly soluble micro-particulated pea isolate 85% or hydrolyzed rice protein with superior cold-water dispersion and low viscosity profile under neutral pH.
2. Plant-Based Meat Alternatives
Formulation Challenge: Replicating real meat fibrous muscle texture, juiciness, and mechanical bite retention.
Ingredient Solution: High-moisture textured vegetable protein (TVP) derived from soy, mung bean, or faba bean isolates with matrix-forming springiness and high oil-holding capacity.
3. Functional Bakery & Snacks
Formulation Challenge: Gluten structure interference, dough hardening, volume loss, excess water absorption.
Ingredient Solution: Enzymatically modified oat protein or pumpkin protein powder providing natural emulsification, crumb softness, and enhanced protein fortification per serving.
Future Trends Shaping Protein Fortification
Key technological shifts and next-generation protein sources defining the market landscape over the next decade.
1. Precision Fermentation & Yeast Isolates
Fermented yeast protein isolates (such as Angeopro Yeast Protein) represent the fast-growing frontier in sustainable nutrition. Yeast proteins offer a near 100% complete PDCAAS score, ultra-low land and water footprint, zero agricultural pesticide exposure, and inherently allergen-free status—making them ideal for clean-label global brands.
2. Upcycled & Specialty Seed Proteins
Circular economy principles are driving high demand for upcycled plant ingredients like sunflower seed protein isolate, hemp protein flour, and pumpkin seed extracts. Rich in natural minerals, zinc, magnesium, and dietary fiber, these seeds provide dual functional benefits: nutritional fortification and clean marketing appeal.
Specialty Protein & Active Supplement Portfolio
Discover additional high-performance plant extracts, yeast isolates, and fiber enhancers engineered for custom product lines.
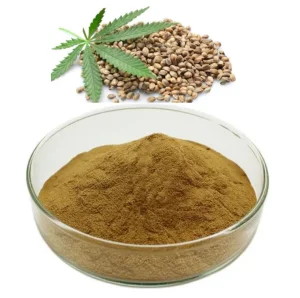
Supply Hemp Kernel Protein 100% Natural Hemp Seed Extract Hemp Protein Powder
View Technical Specs
Food Grade Natural Brown Rice Protein Powder Stabilizers Chewing Gum Bases Nutrition Enhancers
View Technical Specs
BioFlex OEM Private Label Food Grade Vegan 100% Natural Organic Blue-Green Spirulina Algae Extract Antioxidant Immune Support
View Technical Specs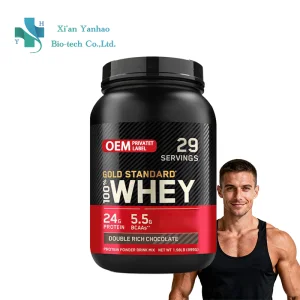
OEM/ODM Customized Natural Concentrate Whey Protein Weight Gain Sport Supplements Whey Protein Powder
View Technical Specs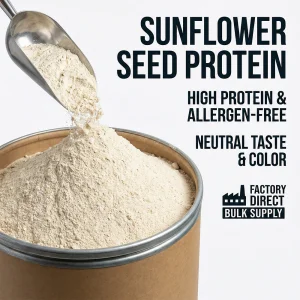
High Purity Natural Sunflower Seed Protein Powder Herbal Extract 50%-90% Extract Health Food Grade Solvent Extraction
View Technical Specs
Tvp Textured Vegetable Protein Tsp with Halal Certification Factory Low Price Textured Soy Protein Raw Materia
View Technical Specs
Dietary Supplement Resistant Dextrin 95% Powder Non-gmo Soluble Corn Fiber
View Technical Specs
Angeopro Yeast Protein Powder Fermented Clean Yeast Protein Powder 99% Pure Yeast Protein Isolate Vegan Protein Powder
View Technical SpecsFrequently Asked Questions (FAQ)
Technical and commercial guidance for purchasing officers, formulators, and brand owners.
What is the typical Minimum Order Quantity (MOQ) for bulk protein isolates?
Standard bulk commercial orders typically start at 500 kg to 1,000 kg per ingredient batch. For specialized OEM/ODM private label packaging or customized trial formulations, initial sample quantities and smaller pilot lots starting from 100 kg can be accommodated.
How does Dongguan Tsrel Biology eliminate off-flavors in plant protein powders?
Through controlled physical washing, proprietary enzymatic debittering, low-temperature vacuum isolation, and advanced deodorization technology, volatile beany off-notes (hexanal compounds) are systematically neutralized, resulting in clean, neutral-tasting powders ideal for unflavored or light-flavored food applications.
Are your protein powders suitable for hypoallergenic and allergen-free product claims?
Yes, we supply a dedicated suite of allergen-free plant proteins including Organic Pea Protein 80%/90%, Pumpkin Seed Protein 60%, Faba Bean Powder 90%, and Fermented Yeast Protein Isolates. These are processed in segregated facilities free from major allergens such as soy, wheat gluten, dairy, and tree nuts.
What testing and documentation are supplied with each export shipment?
Every commercial shipment includes a comprehensive Certificate of Analysis (COA) specifying protein content, moisture, ash, heavy metals, microbial parameters, and particle size distribution. Additionally, Technical Data Sheets (TDS), Safety Data Sheets (SDS), Allergen Statements, and Non-GMO certifications are provided for full regulatory compliance.
What is the typical shelf life and recommended storage condition for protein isolates?
Our plant protein isolates carry a standard 24-month shelf life from the date of manufacture when stored unopened in original, sealed multi-wall moisture-barrier packaging in a dry, cool environment (temperatures below 25°C and relative humidity under 60%).